

Cold forging squeezes metal into a precision die at room temperature. The result is a stronger part, closer to finished size, with far less scrap and machining. Knuckle joint presses deliver their highest force and slowest ram speed right at the bottom of the stroke, exactly where cold forging does its work. Sutherland's KNP Series pairs that mechanism with I-PRESS® controls to protect tooling and hold accuracy at volume.
Think of pressing modeling clay between two shaped tools. The clay flows into their shape. Cold forging works the same way with steel, aluminum, copper and brass, using hundreds to thousands of tons of force. A near-net-shape part leaves the press close to its final dimensions. A net-shape part needs no machining at all on its finished features.
Bar or wire cut into slugs of tightly controlled weight.
Annealed, coated and lubricated so metal flows without cracking.
A feeder, robot or transfer places the slug in the die.
The ram drives metal into the die cavity, in one or more stages.
The part is ejected and checked for dimensions and quality.
Heat treat or machine only the surfaces the spec requires.
A crank press moves the ram with general-purpose motion. A knuckle joint linkage slows the ram and multiplies mechanical advantage as it nears bottom dead center, exactly where metal is packed into the die.
Compresses metal fully into precision die cavities.
A gentler approach means less shock on expensive tooling.
Controlled final motion, backed by a rigid frame and good die design.
Built for high-volume runs with proper feeding and monitoring.
| Property | Effect | Why It Matters |
|---|---|---|
| Yield & Tensile Strength | Up | Stronger components |
| Hardness | Up | Better wear resistance |
| Grain Flow | Aligned | Can improve fatigue life |
| Dimensional Accuracy | Excellent | Less machining |
| Ductility | Down | Process must respect formability |
Aerospace and automotive high-strength fasteners, transmission and steering parts, bearings and races, hubs and rings, gear blanks, heavy equipment and electrical hardware. Low-carbon steel, aluminum and copper forge best cold. Alloy and stainless steels work with the right process design.
Engineered for high-volume precision metal forming, the KNP Series combines the mechanical advantages of knuckle joint technology with the advanced monitoring, die protection, production management and automation capabilities of Sutherland's I-PRESS® controls on the AB PLUS® platform.

On a KNP, I-PRESS® turns every stroke into a measurable productivity and tooling-protection advantage.
Detects abnormal forging loads
Flags changes in material, lubrication and die condition
Catches dimensional drift and thermal change
Guards against misfeeds, double blanks and stuck parts
Protects high-value forging dies
Faster, more repeatable changeovers
Supports quality tracking and preventive maintenance
Coordinates feeding, transfer, ejection and inspection
The biggest opportunity is not simply selling a 1,000-ton press. It is helping manufacturers convert a costly machining or multistep process into a high-volume, near-net-shape forging operation.
Still machining fasteners, gear blanks or hubs from bar stock? Our team will tell you if it can be cold forged near net shape on a KNP.


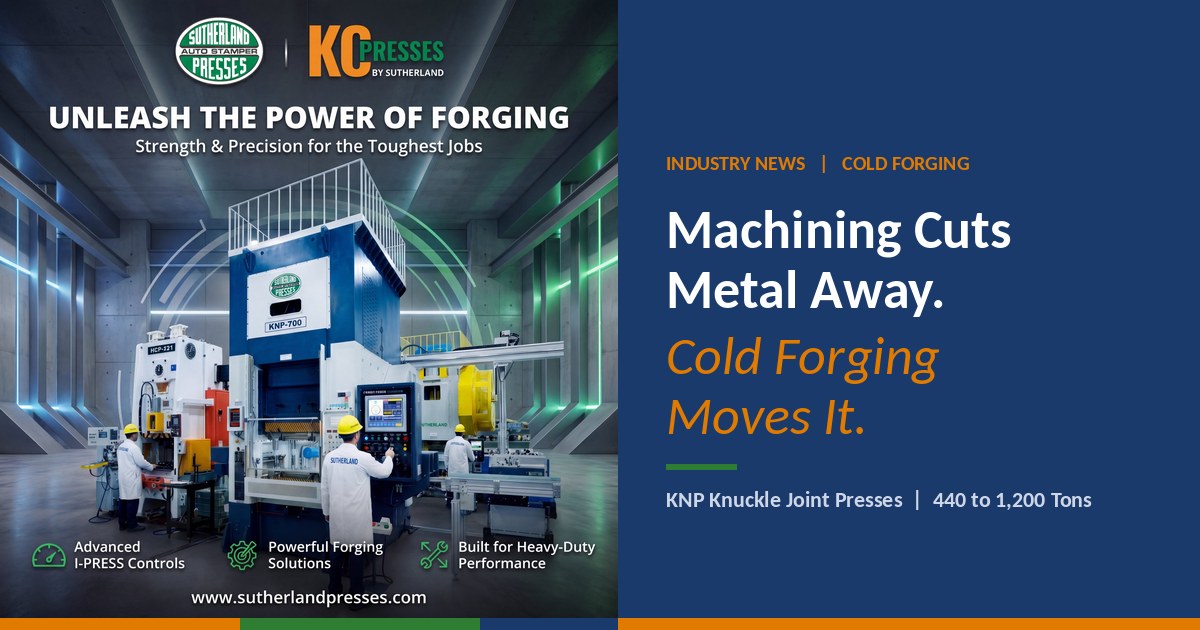
Cold forging squeezes metal into a precision die at room temperature. The result is a stronger part, closer to finished size, with far less scrap and machining. Knuckle joint presses deliver their highest force and slowest ram speed right at the bottom of the stroke, exactly where cold forging does its work. Sutherland's KNP Series pairs that mechanism with I-PRESS® controls to protect tooling and hold accuracy at volume.
Think of pressing modeling clay between two shaped tools. The clay flows into their shape. Cold forging works the same way with steel, aluminum, copper and brass, using hundreds to thousands of tons of force. A near-net-shape part leaves the press close to its final dimensions. A net-shape part needs no machining at all on its finished features.
Bar or wire cut into slugs of tightly controlled weight.
Annealed, coated and lubricated so metal flows without cracking.
A feeder, robot or transfer places the slug in the die.
The ram drives metal into the die cavity, in one or more stages.
The part is ejected and checked for dimensions and quality.
Heat treat or machine only the surfaces the spec requires.
A crank press moves the ram with general-purpose motion. A knuckle joint linkage slows the ram and multiplies mechanical advantage as it nears bottom dead center, exactly where metal is packed into the die.
Compresses metal fully into precision die cavities.
A gentler approach means less shock on expensive tooling.
Controlled final motion, backed by a rigid frame and good die design.
Built for high-volume runs with proper feeding and monitoring.
| Property | Effect | Why It Matters |
|---|---|---|
| Yield & Tensile Strength | Up | Stronger components |
| Hardness | Up | Better wear resistance |
| Grain Flow | Aligned | Can improve fatigue life |
| Dimensional Accuracy | Excellent | Less machining |
| Ductility | Down | Process must respect formability |
Aerospace and automotive high-strength fasteners, transmission and steering parts, bearings and races, hubs and rings, gear blanks, heavy equipment and electrical hardware. Low-carbon steel, aluminum and copper forge best cold. Alloy and stainless steels work with the right process design.
Engineered for high-volume precision metal forming, the KNP Series combines the mechanical advantages of knuckle joint technology with the advanced monitoring, die protection, production management and automation capabilities of Sutherland's I-PRESS® controls on the AB PLUS® platform.
On a KNP, I-PRESS® turns every stroke into a measurable productivity and tooling-protection advantage.
Detects abnormal forging loads
Flags changes in material, lubrication and die condition
Catches dimensional drift and thermal change
Guards against misfeeds, double blanks and stuck parts
Protects high-value forging dies
Faster, more repeatable changeovers
Supports quality tracking and preventive maintenance
Coordinates feeding, transfer, ejection and inspection
The biggest opportunity is not simply selling a 1,000-ton press. It is helping manufacturers convert a costly machining or multistep process into a high-volume, near-net-shape forging operation.
Still machining fasteners, gear blanks or hubs from bar stock? Our team will tell you if it can be cold forged near net shape on a KNP.


